
Metal conveyor belt systems play an essential role in modern manufacturing, food processing, and industrial material handling. Businesses rely on durable, efficient conveyor solutions to move products safely, maintain consistent production, and reduce operational delays. wire belt Company is an excellent example of a specialist in designing, manufacturing, and installing customized conveyor belts for food processing and industrial applications. Through tailored solutions, technical support, belt surveys, training, and maintenance tools, the company helps businesses improve efficiency, minimize downtime, extend equipment life, and optimize overall system performance.
Understanding Metal Conveyor Belt Systems
Conveyor systems are designed to transport products, materials, and components between different stages of a production process. metal conveyor belts are particularly valuable in environments where strength, durability, temperature resistance, and reliable operation are essential. Unlike some alternative belt materials, metal belts can withstand demanding working conditions, making them suitable for applications involving heat, moisture, cleaning chemicals, and heavy loads, depending on their design and material composition.
These systems are available in several configurations, including flat wire belts, balanced weave belts, and other specialized mesh designs. Each configuration offers distinct advantages depending on the product being transported, the operating environment, and the requirements of the production line.
Selecting the right conveyor belt helps businesses achieve smoother material flow, maintain consistent product quality, and reduce interruptions caused by unsuitable equipment.
Applications Across Food Processing and Industry
Metal conveyor belts are widely used in food manufacturing because they can support efficient product movement through processing, cooking, cooling, freezing, and cleaning operations. Open-mesh designs allow air, liquids, and heat to pass through the belt, making them useful for applications that require uniform heat transfer or effective drainage.
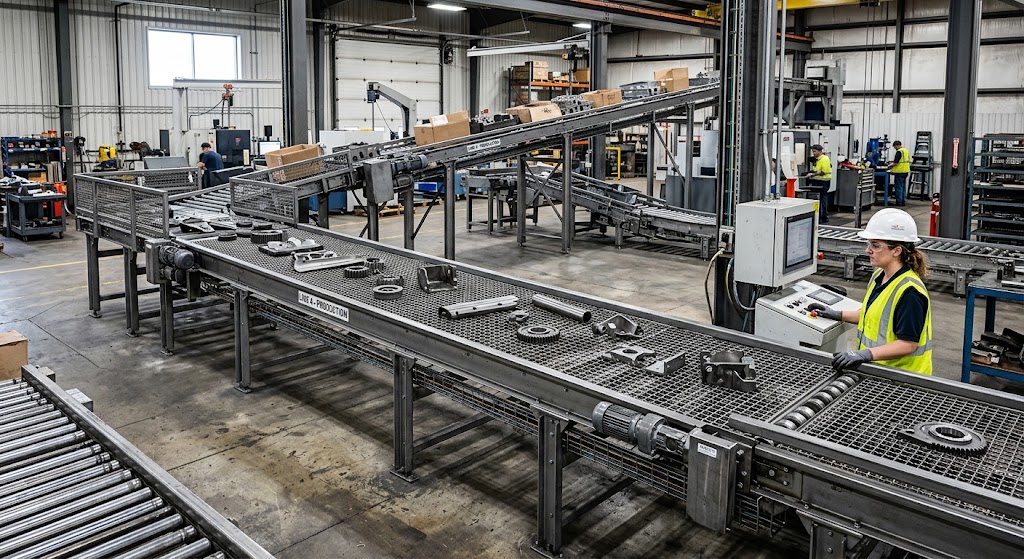
In industrial environments, these belts support manufacturing, assembly, packaging, and material transfer. Their strength and resistance to demanding conditions make them suitable for moving components through production stages where reliability is essential.
Industries that commonly benefit from metal conveyor systems include:
-
Food processing: Transporting products through baking, frying, cooling, freezing, and washing operations.
-
Automotive manufacturing: Moving components through assembly, finishing, and heat-treatment processes.
-
Electronics production: Supporting controlled product movement during manufacturing and assembly.
-
Packaging operations: Maintaining a consistent flow of products between processing and packaging equipment.
-
Industrial manufacturing: Handling components and materials in environments with demanding operating conditions.
Choosing a suitable belt design for each application helps businesses maintain productivity while meeting their operational and quality requirements.
Choosing the Right Wire Belt for Your Operation
Selecting the appropriate wire belt involves more than comparing dimensions or materials. Businesses need to consider product characteristics, operating temperatures, load requirements, belt speed, cleaning procedures, and the layout of the conveyor system.
Different belt constructions provide different levels of flexibility, strength, openness, and product support. For example, open-mesh designs can improve airflow in thermal processing applications, while more closely spaced wire configurations may be better suited to transporting smaller products.
Other important considerations include corrosion resistance, drive compatibility, belt tracking, and the frequency of maintenance required. A carefully selected belt can reduce product damage, improve production consistency, and help prevent premature equipment wear.
Working with an experienced conveyor specialist can simplify this process. Technical assessments and application-specific recommendations help businesses identify suitable equipment and avoid problems associated with poorly matched conveyor components.
How Custom Conveyor Solutions Improve Efficiency
Standard conveyor belts may not meet every production requirement. Differences in product size, processing conditions, available floor space, and production speeds often require specialized designs.
Custom conveyor solutions allow businesses to match belt construction and system configuration to their specific applications. Adjustments to belt width, mesh pattern, material selection, and operating characteristics can help improve product handling and integrate equipment more effectively into existing production lines.
A well-designed system can also reduce unnecessary transfers between machines, improve workflow, and minimize bottlenecks. These improvements are particularly valuable in facilities where even short production interruptions can affect output and delivery schedules.
Beyond initial design and installation, technical support helps businesses identify opportunities to improve existing conveyor systems. Professional guidance can assist with troubleshooting, performance assessments, and selecting appropriate replacement components.
Reducing Downtime Through Maintenance and Technical Support
Unexpected conveyor failures can disrupt production, increase labor costs, and create delays throughout a facility. Preventive maintenance is therefore an important part of managing material handling equipment.
Regular inspections can identify problems such as damaged wires, worn components, incorrect belt tracking, and excessive tension before they develop into more serious failures. Cleaning procedures should also be appropriate for the belt material and operating environment, particularly in food processing facilities where hygiene is a priority.
Several maintenance practices can help extend conveyor equipment life:
-
Schedule routine inspections: Examine belts, drives, sprockets, and other critical components for signs of wear or damage.
-
Monitor belt tracking: Correct alignment issues early to reduce uneven wear and operational interruptions.
-
Follow appropriate cleaning procedures: Remove accumulated debris and residue using methods suitable for the belt’s application.
-
Train maintenance personnel: Ensure employees understand correct operating procedures and can recognize early warning signs.
-
Use suitable maintenance tools: Apply the correct tools and techniques when inspecting, adjusting, or repairing conveyor systems.
-
Keep maintenance records: Document inspections, repairs, and recurring issues to identify opportunities for improvement.
Combining these practices with professional technical support helps businesses make informed maintenance decisions and reduce avoidable downtime.
The Importance of Belt Surveys and Employee Training
Belt surveys provide useful information about the condition and performance of an existing conveyor system. By evaluating belt dimensions, operating conditions, wear patterns, and installation requirements, specialists can help businesses identify potential issues and determine whether adjustments or replacements are necessary.
These assessments are especially useful when a production facility experiences recurring belt problems, changes its manufacturing processes, or plans to upgrade its equipment.
Employee training is equally important. Operators and maintenance teams who understand correct belt handling, installation requirements, cleaning procedures, and routine inspection techniques are better equipped to maintain reliable operations.
Specialized maintenance tools and practical guidance can further support these efforts. Together, belt surveys, training, and ongoing technical assistance help businesses protect their equipment investments and maintain consistent production performance.
Improving Long-Term Material Handling Performance
Effective material handling depends on more than installing a durable conveyor belt. Businesses must consider equipment selection, system integration, maintenance planning, employee knowledge, and ongoing performance evaluation.
Metal conveyor belts offer a versatile solution for applications that demand strength, reliability, and resistance to challenging operating conditions. When combined with an appropriate conveyor design and a proactive maintenance strategy, they can help improve productivity, reduce product handling problems, and support more efficient manufacturing processes.
Partnering with an experienced supplier such as Wire Belt Company can help organizations evaluate their requirements and develop solutions suited to their operations. With customized conveyor systems, technical support, belt surveys, training, and maintenance resources, businesses can improve equipment reliability and make better use of their production capacity.
Ultimately, investing in the right conveyor technology and maintaining it properly helps create a more dependable material handling operation, supporting long-term efficiency, reduced downtime, and sustainable business performance.